Advanced technologies engineered to maintain freshness, reduce waste and enhance the in-store experience across a wide range of environments.
✓ Systems can operate independently or be combined for maximum performance and results.
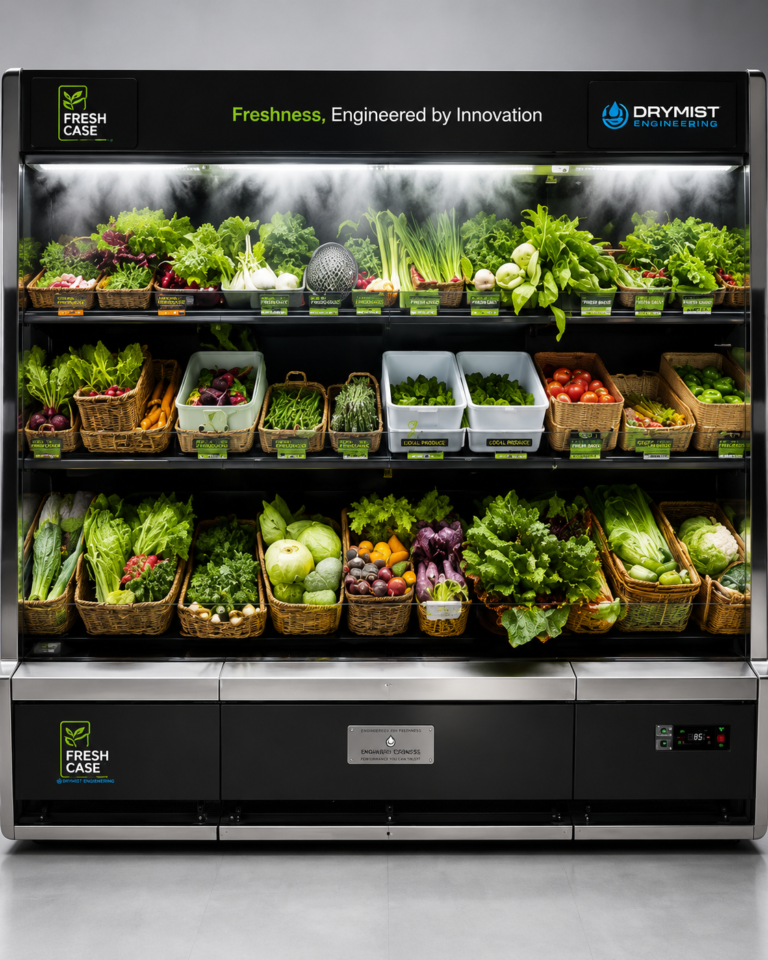
Modular ambient displays that enhance freshness, improve presentation and reduce shrinkage
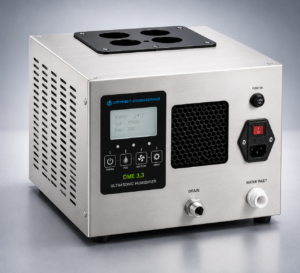
Advanced ultrasonic humidification delivering ultra-fine dry fog for maximum freshness and product quality
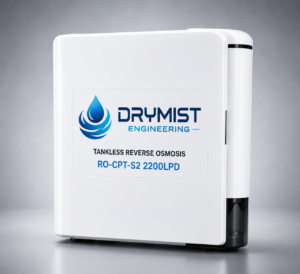
High-performance RO filtration providing clean, reliable water for optimal system performance
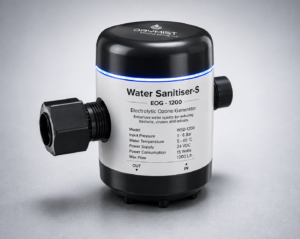
Electrolytic Ozone Generation improves water quality, supports sanitation and freshness management
Expert servicing, genuine parts and technical support to keep your systems performing at their best
Advanced solutions engineered to improve freshness, reduce waste and deliver reliable performance across retail and commercial environments
Maintain optimal conditions to help extend shelf life and preserve product quality
Minimise product loss through improved environmental control
Maintain fresher, more appealing displays that enhance the customer experience
Engineered for dependable performance, efficiency and long-term operation
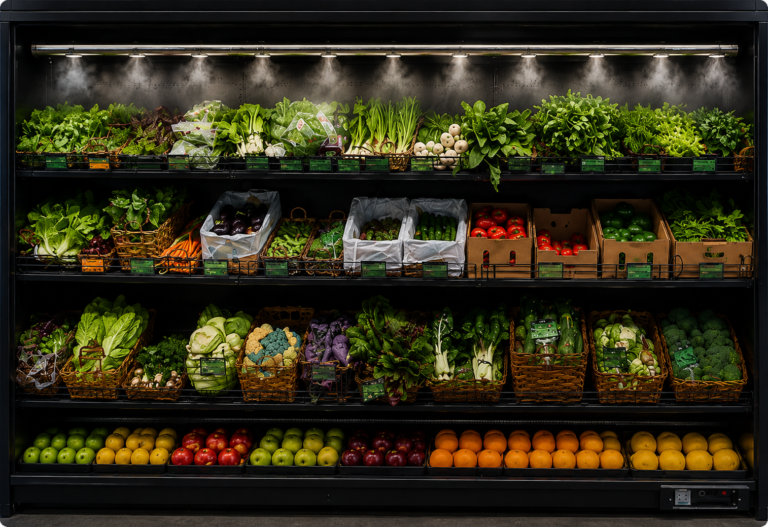
Modular ambient display systems combining ultrasonic humidification, water purification and EOG technology to maintain freshness, improve presentation and significantly reduce energy consumption
✓ Ambient operation – no refrigeration
✓ Modular & scalable design
✓ High humidity performance – 85–90% RH
✓ Significant energy-saving potential
✓ Ideal for produce, floral and more
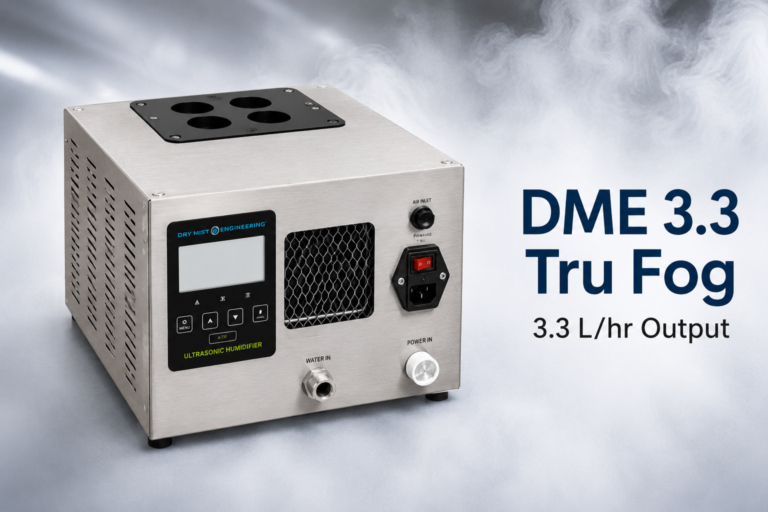
Advanced ultrasonic humidification systems producing ultra-fine dry fog to maintain optimal humidity, reduce moisture loss and help preserve product freshness and quality
✓ Consistent humidity performance
✓ Stainless steel construction
✓ Programmable system control
✓ Range of capacities to suit different applications
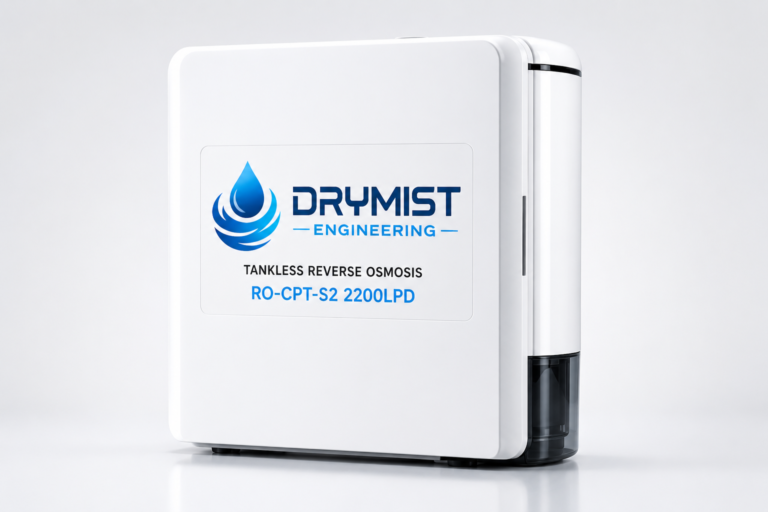
High-performance reverse osmosis filtration systems delivering clean, purified water to support reliable system performance and long-term operation
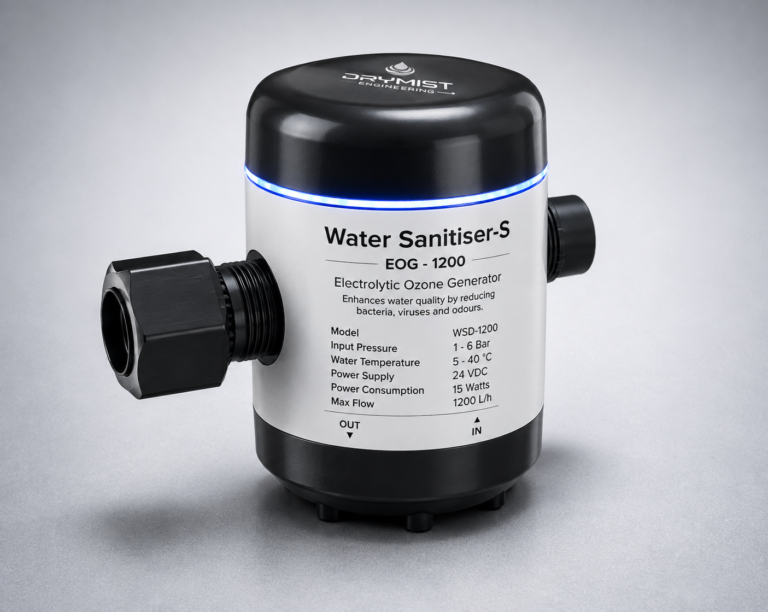
Electrolytic Ozone Generation (EOG) introduces aqueous ozone into the water system to support water quality, reduce contamination and help maintain freshness throughout the display
Comprehensive servicing, preventative maintenance and technical support to keep DME systems operating reliably and performing at their best.
Whether you’re upgrading existing displays or planning a new installation, Dry Mist Engineering can deliver a tailored solution to suit your store, product range and operational needs
© 2026 Dry Mist Engineering Pty Ltd. All Rights Reserved